
‹
›
OEM Service Process
Complete the cooperation in four simple steps, with a professional team providing full support throughout the process.
Confirmation of product type, specifications, quantity, and special requirements
Provide a complete solution and detailed quotation
Make samples and adjust them to satisfaction
Mass production delivery based on confirmed samples
Product Detail
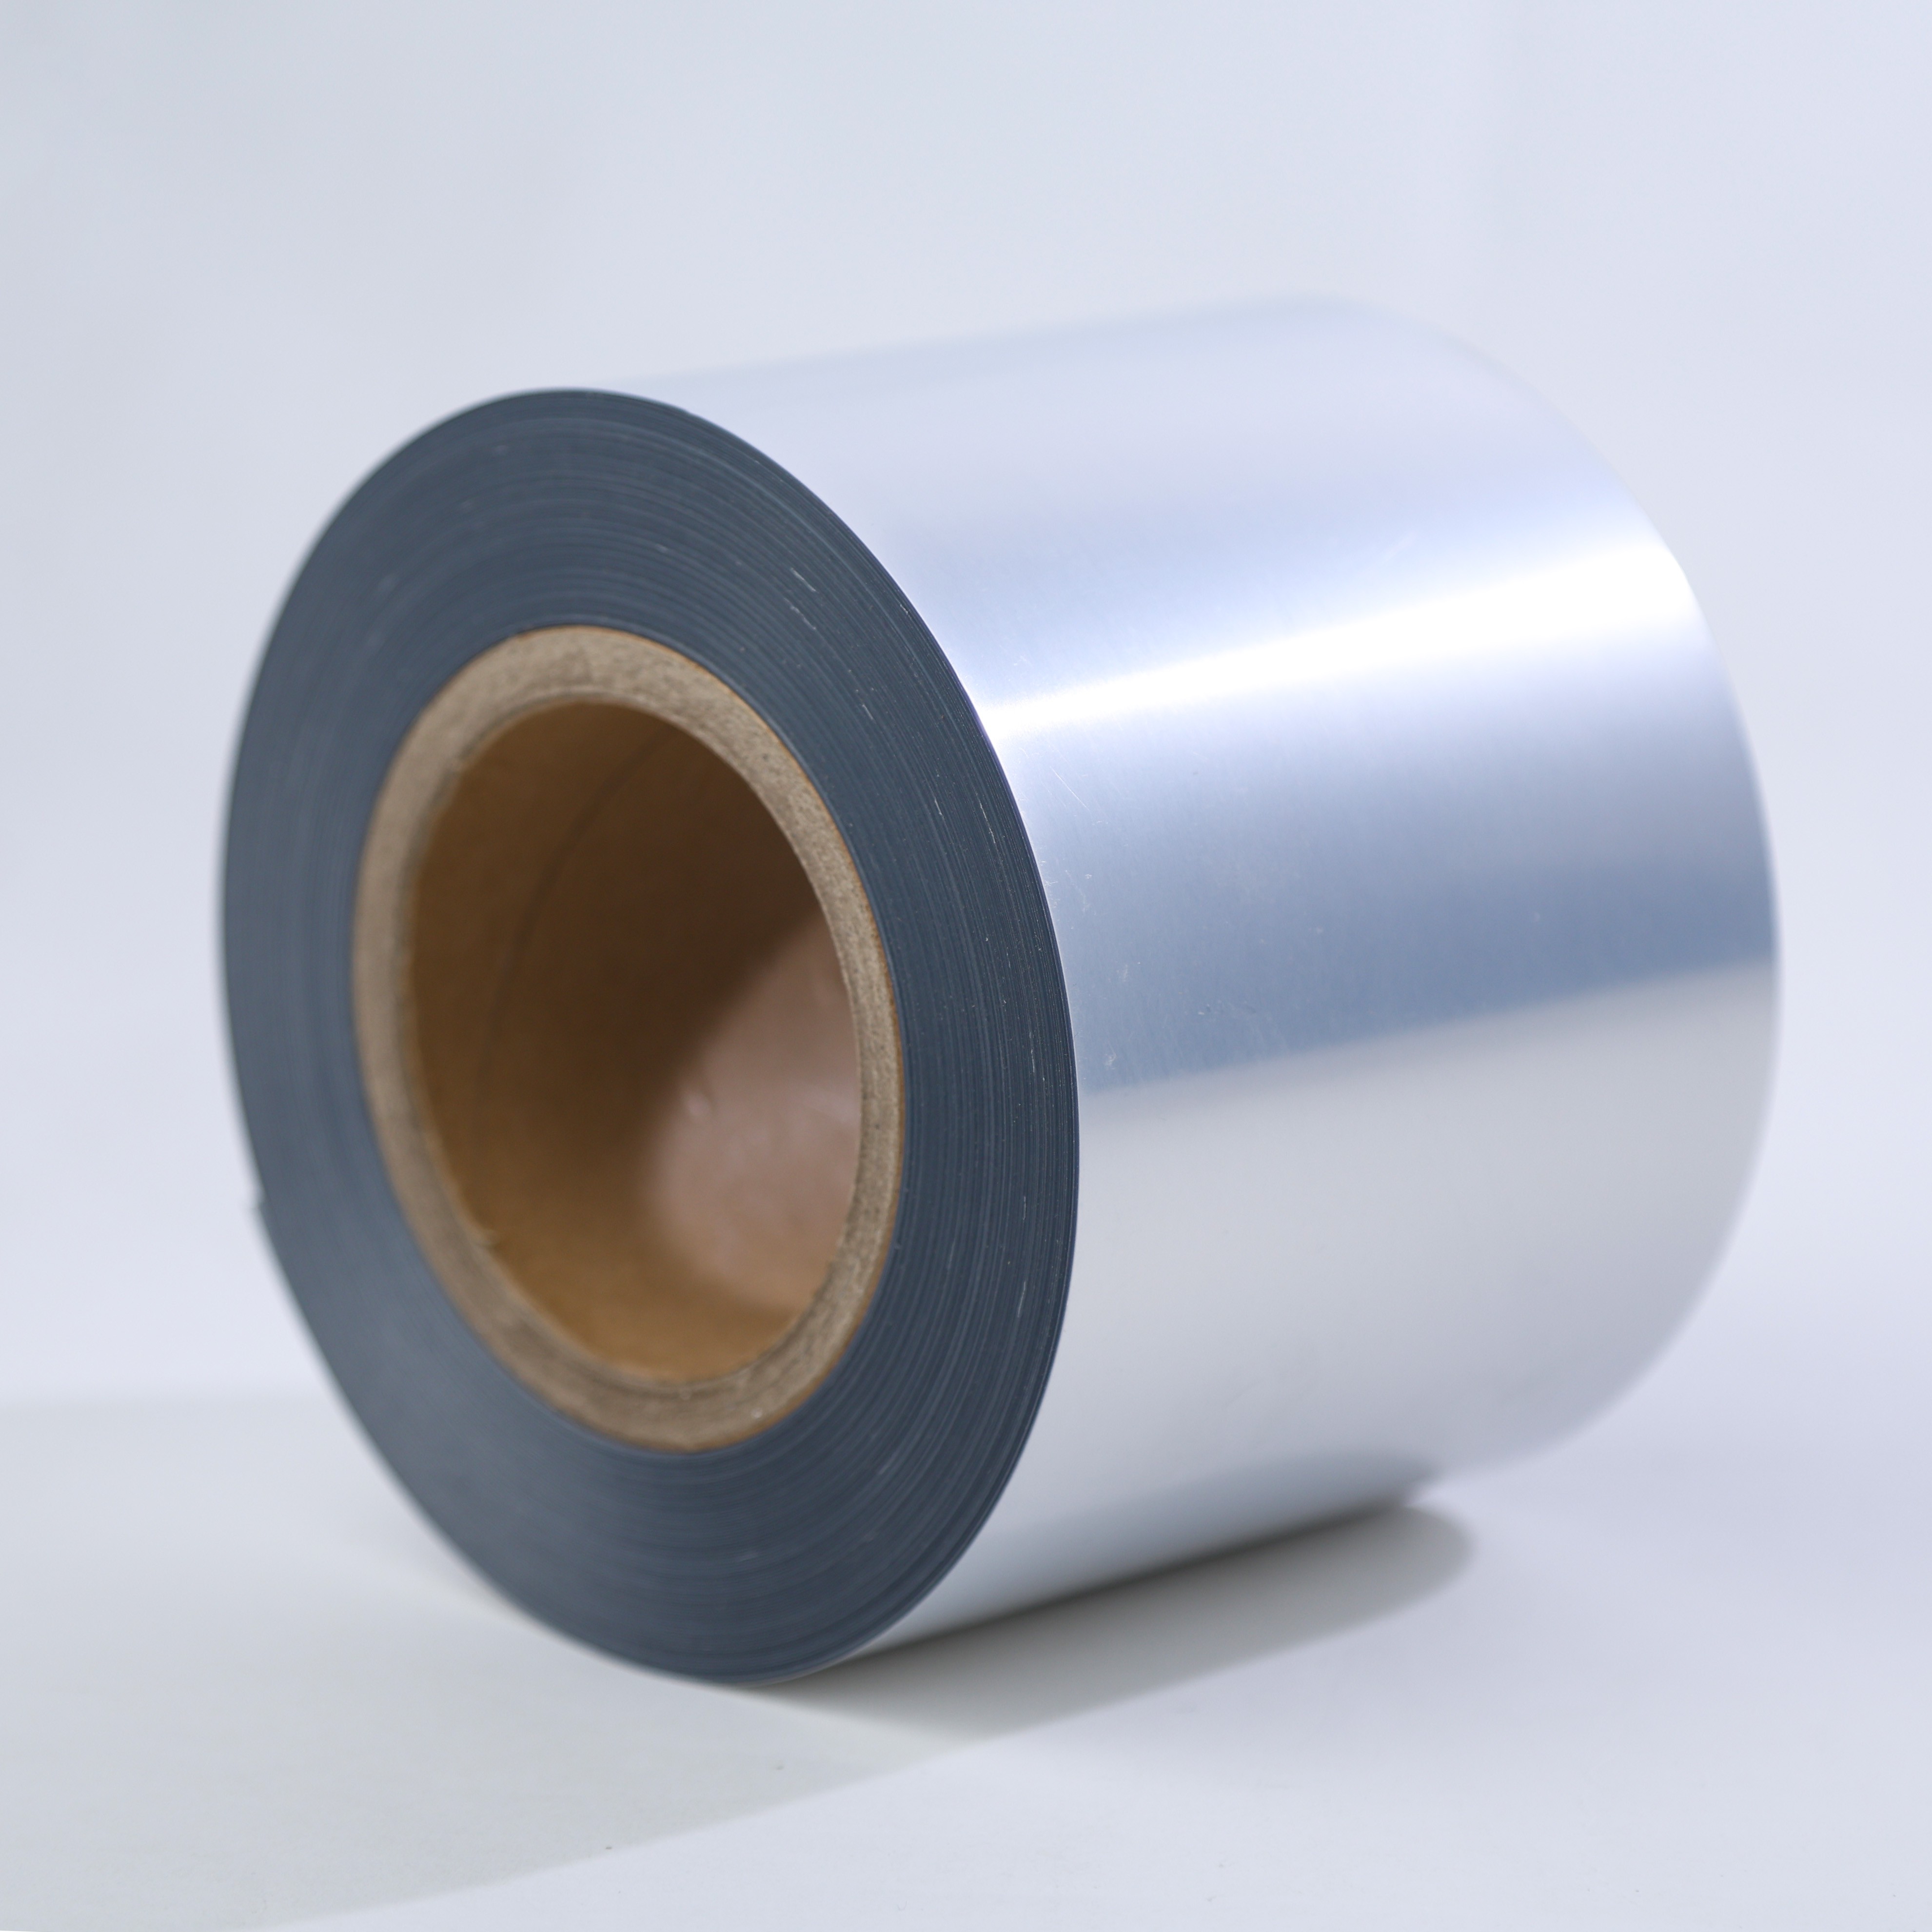
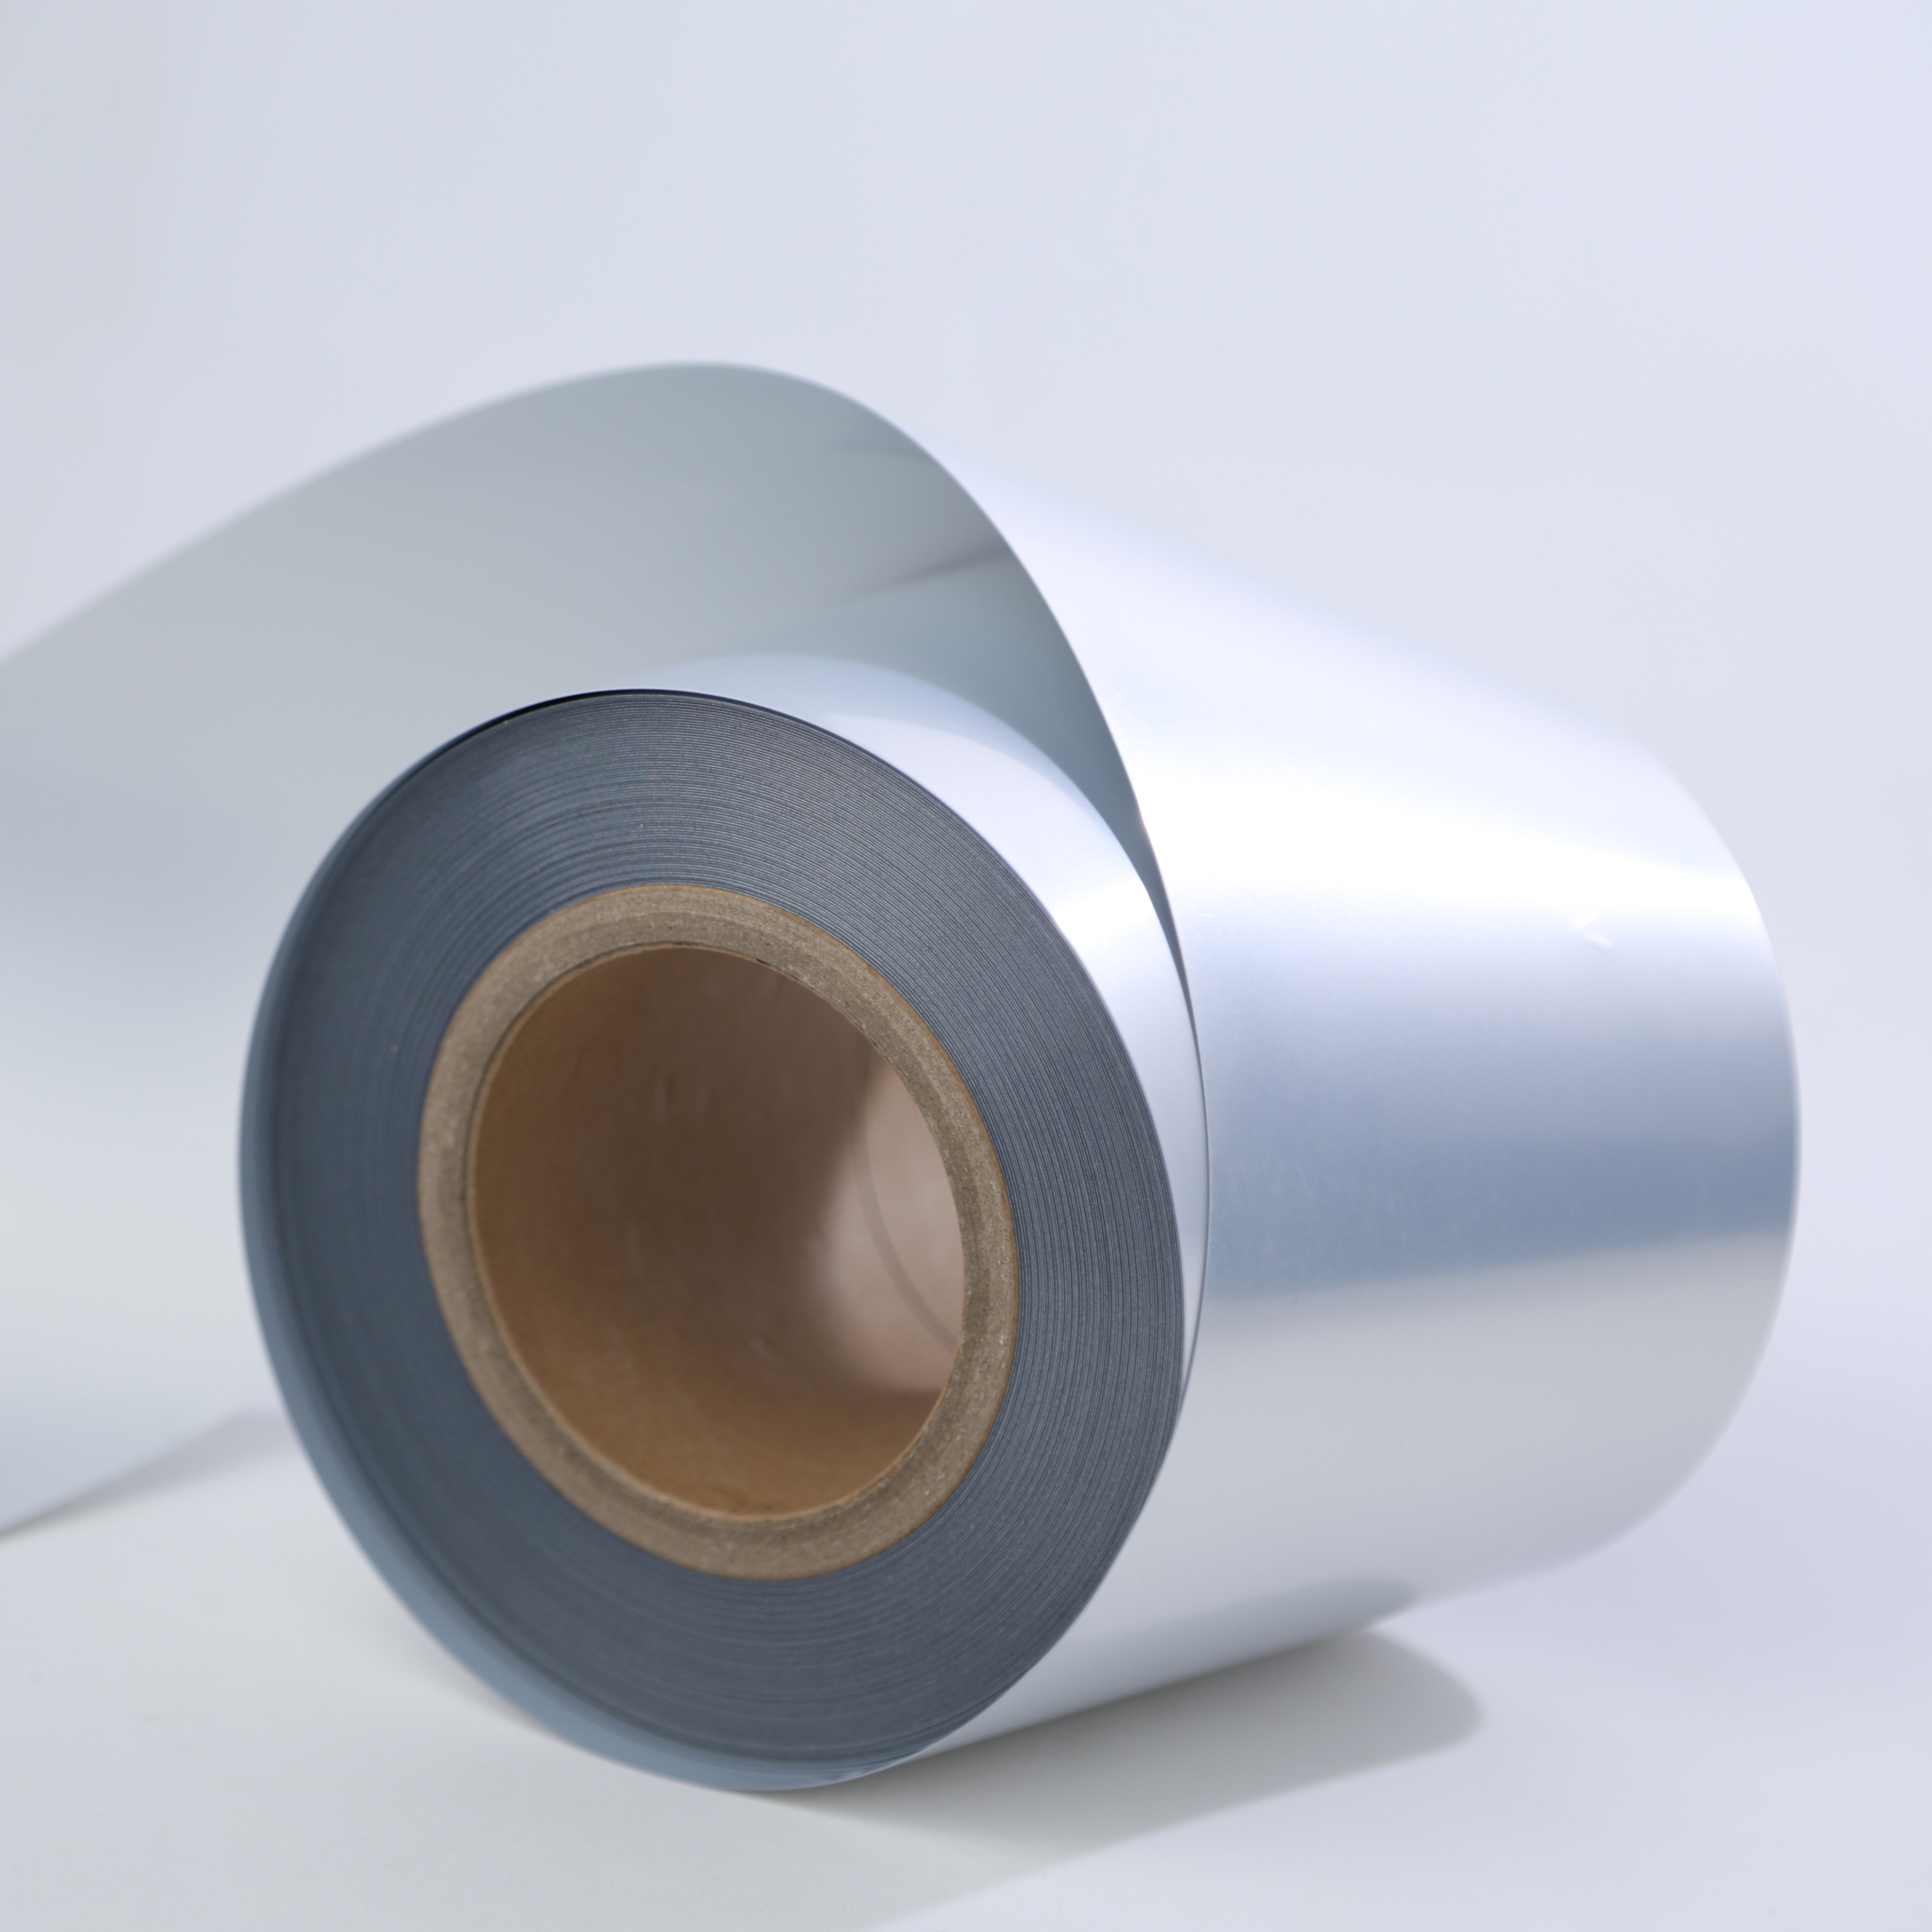
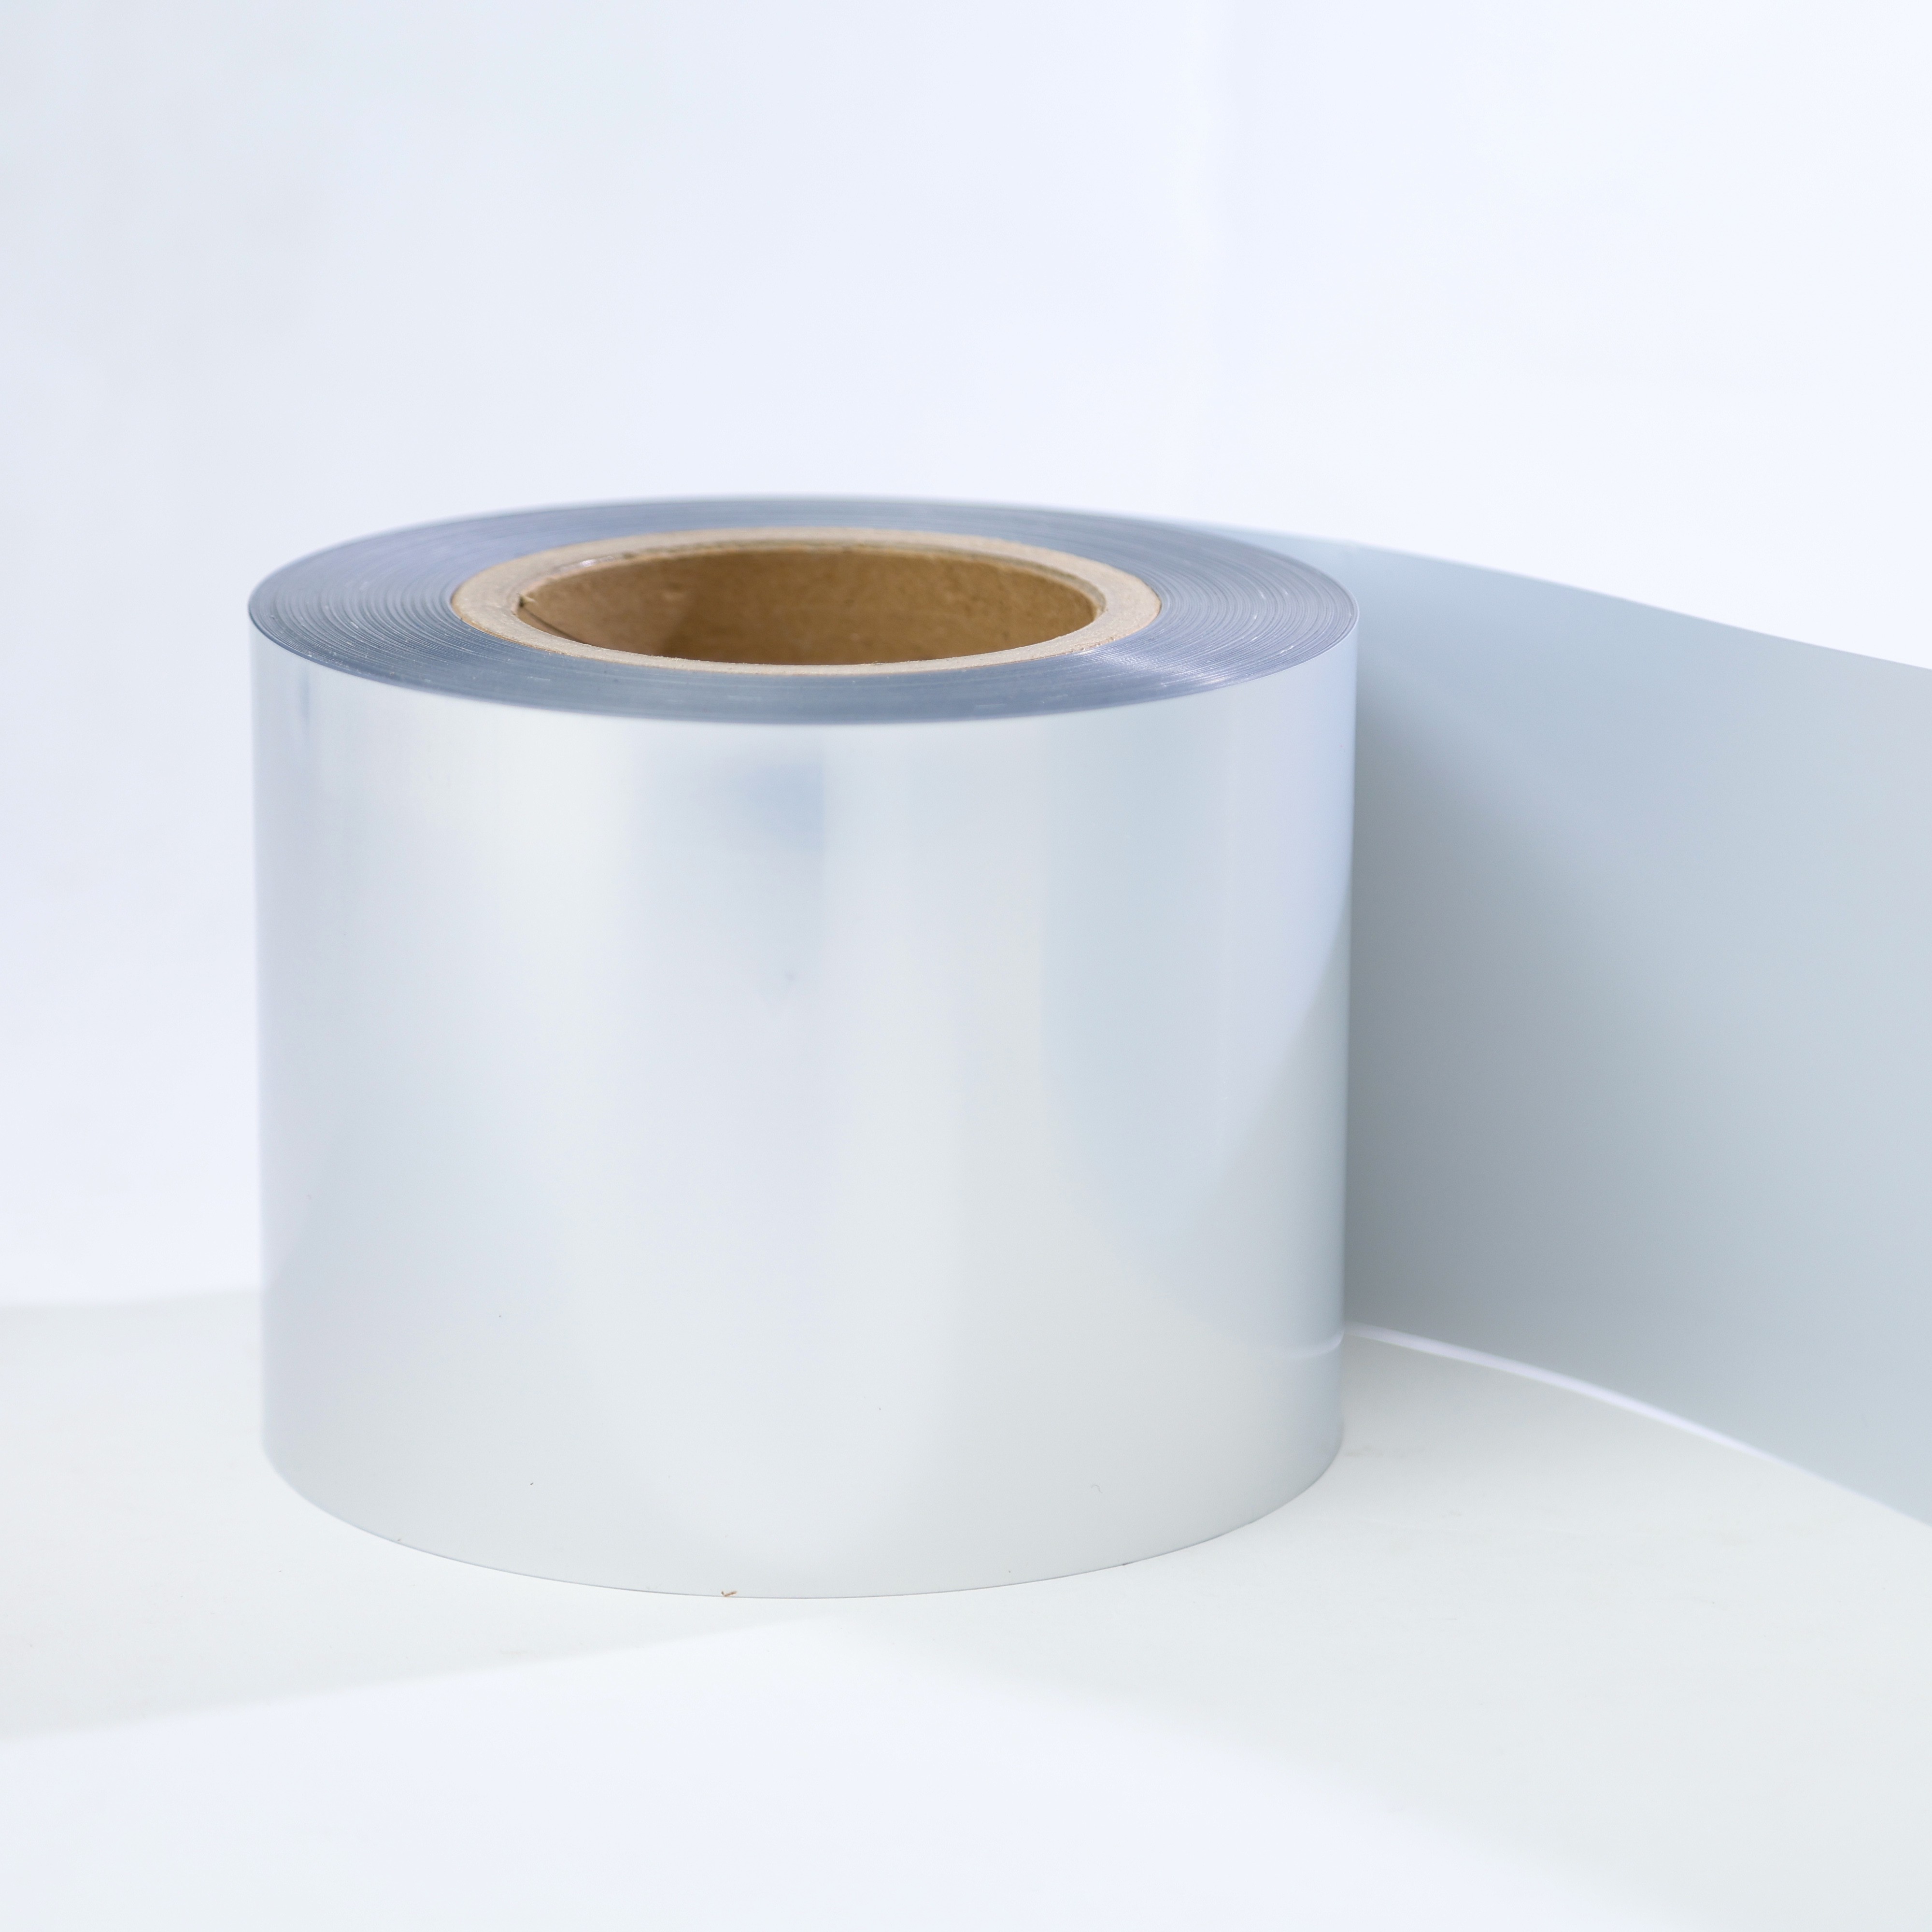
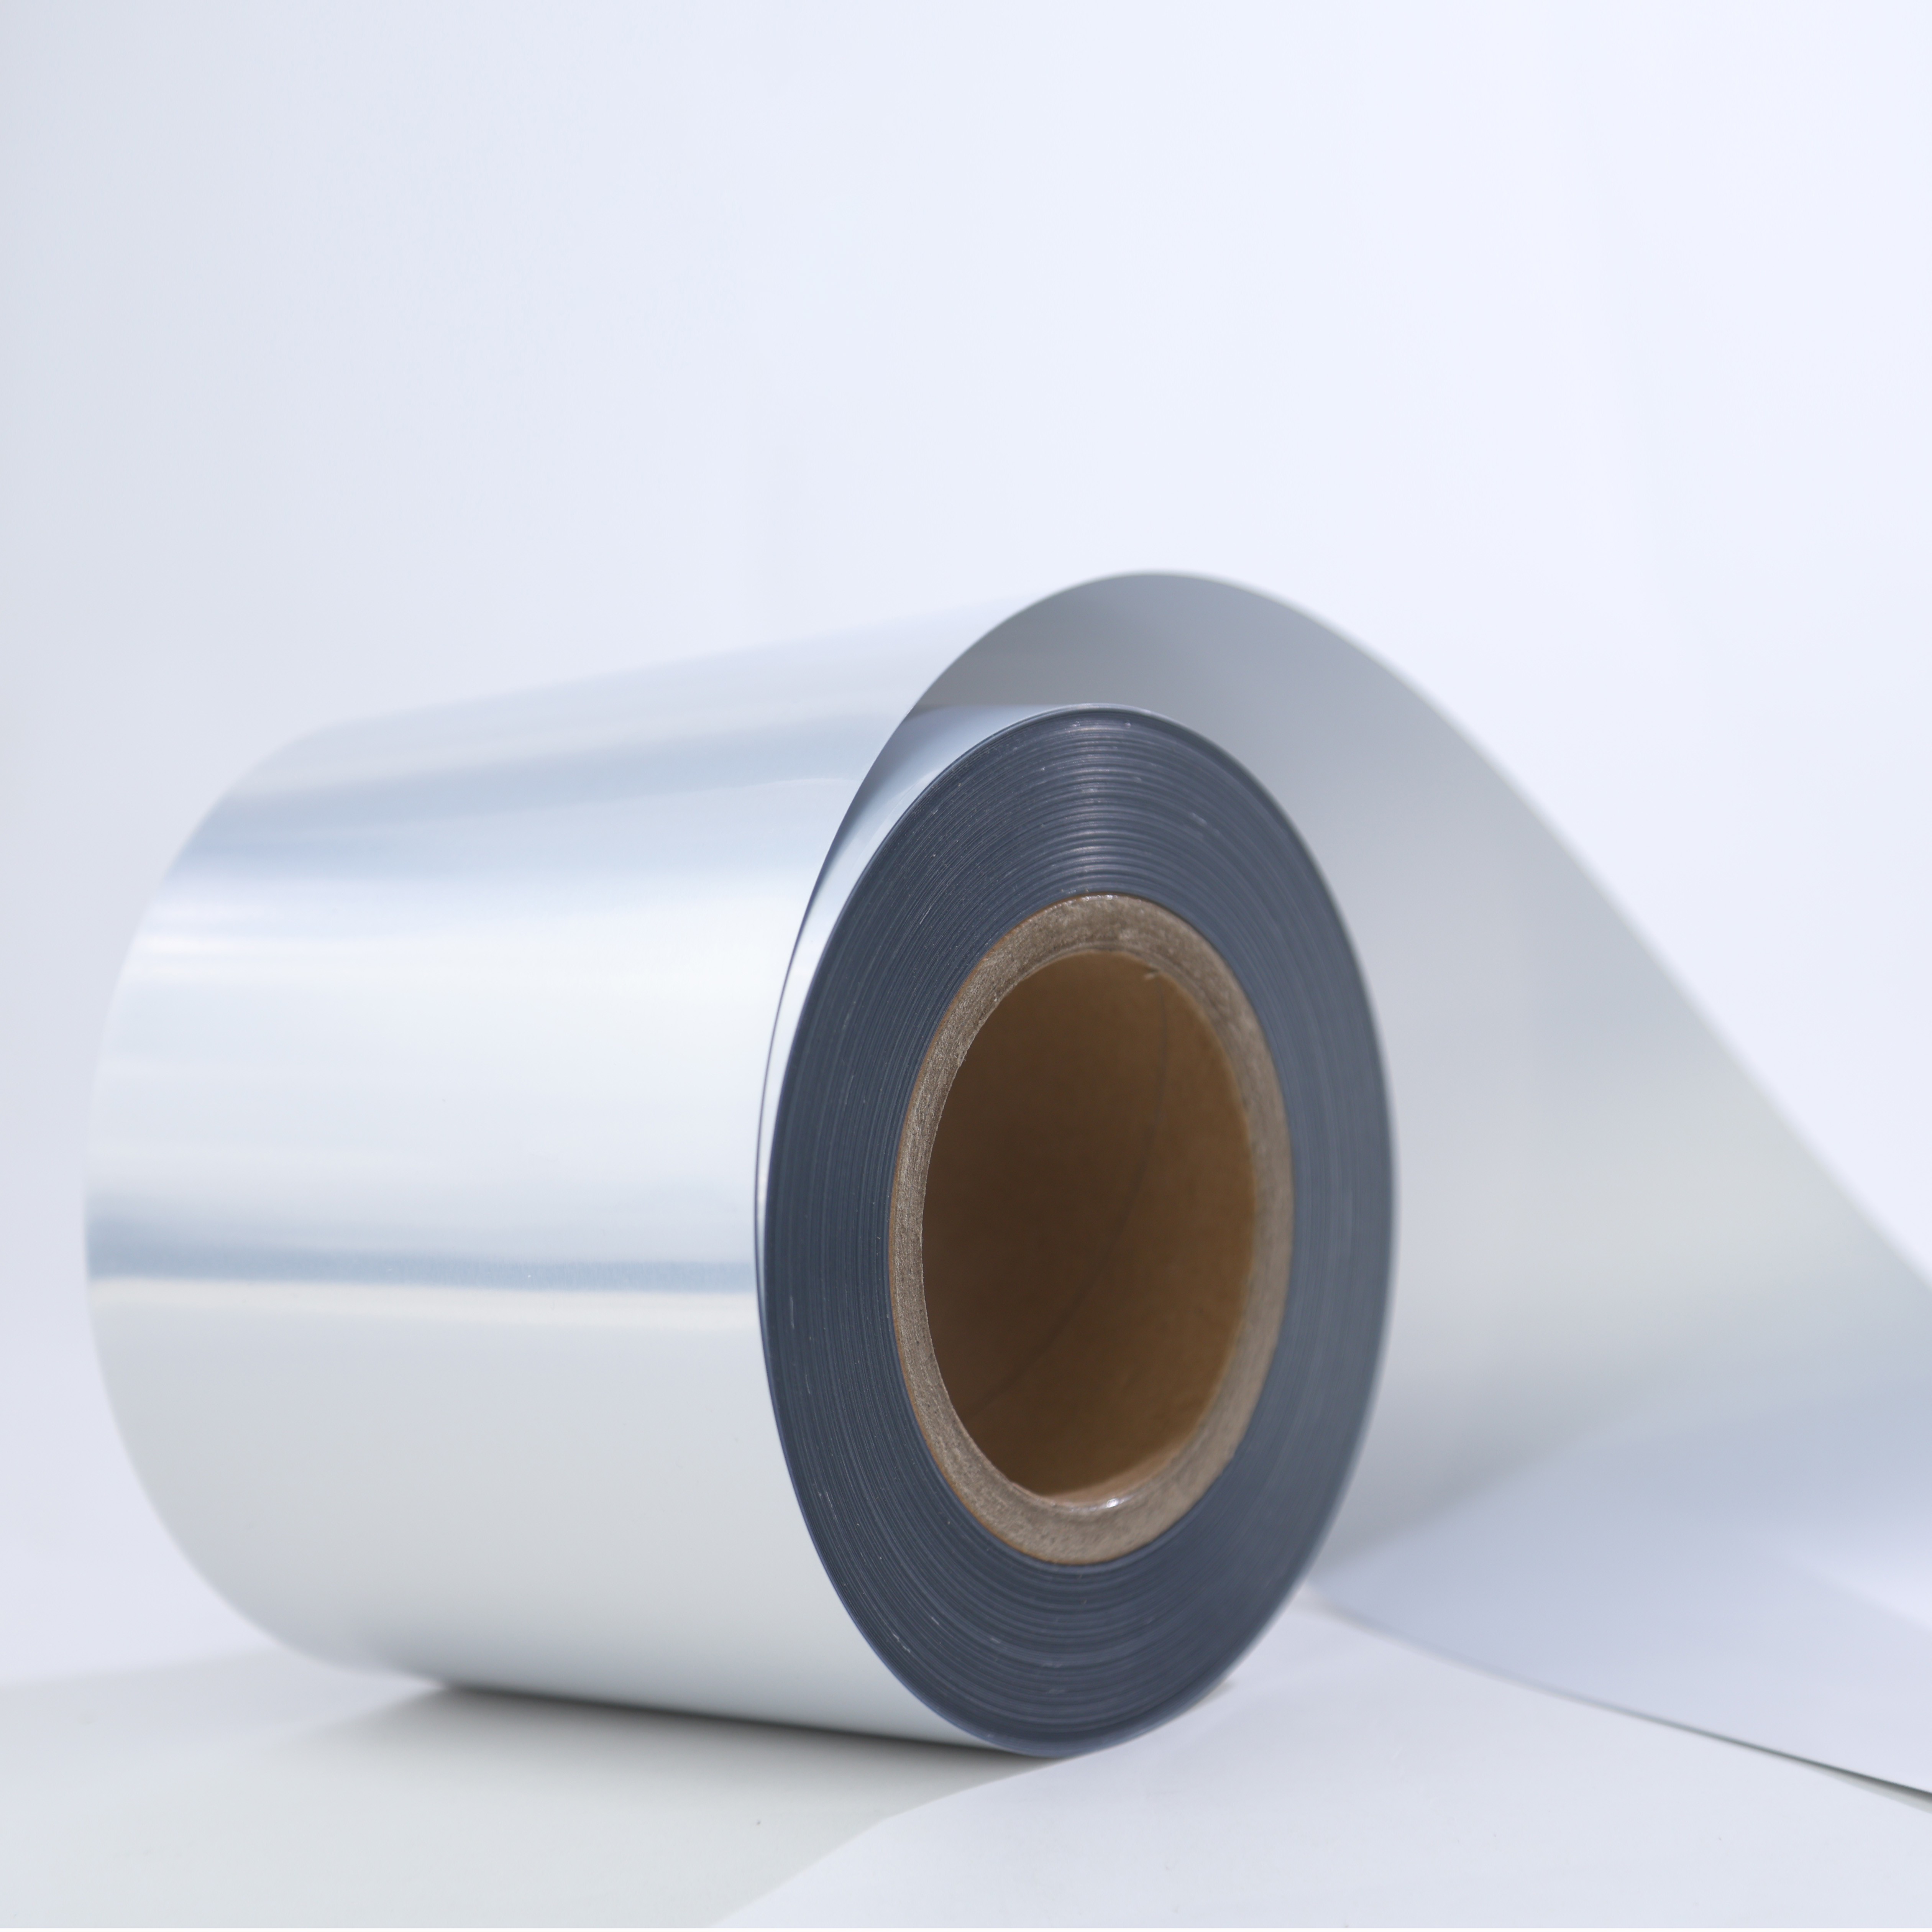
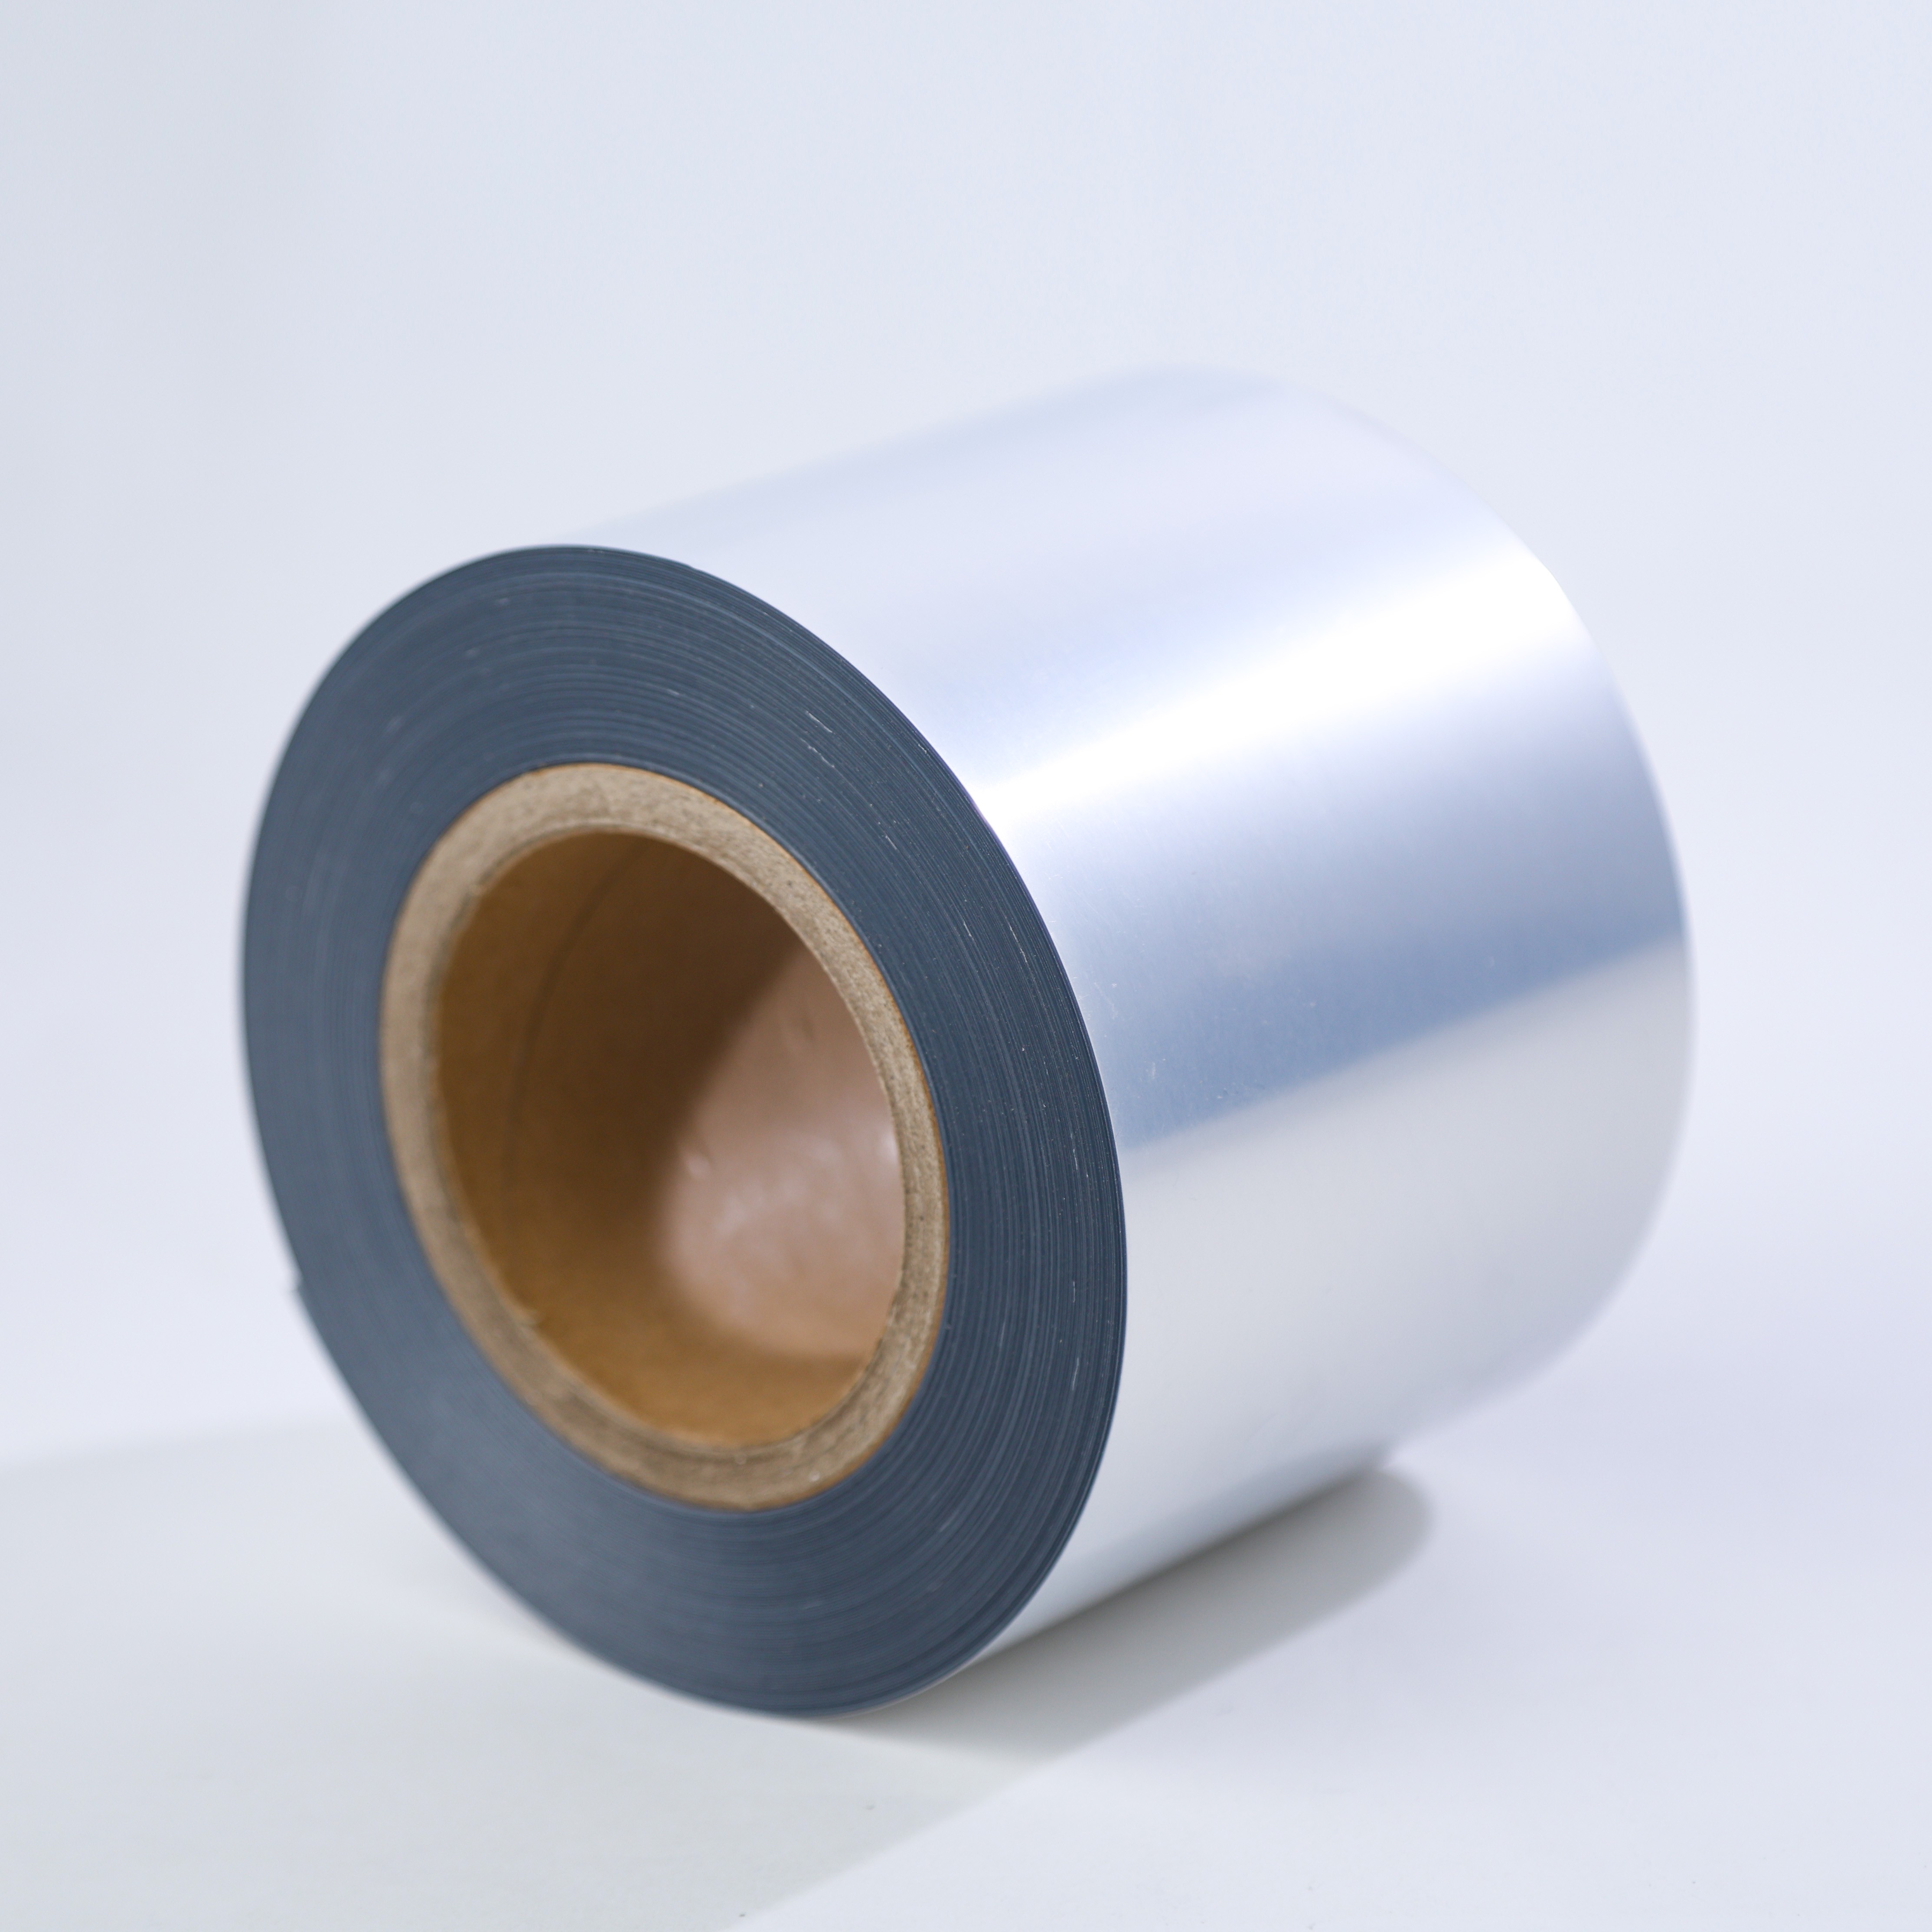
ABL-Silver is a premium packaging solution built around an aluminium foil core as its primary functional barrier. The designation “ABL” stands for Aluminum Barrier Laminate, reflecting the material’s fundamental architecture. Through precision multi-layer co-extrusion and lamination technology, the product synergistically combines the inherent physical protection of aluminium foil with the processing flexibility of polymeric substrates, offering a dependable protective enclosure for high-value and environment-sensitive contents.
The total thickness of ABL-Silver is configurable within a broad range of 175 μm to 425 μm, while the aluminium foil layer itself can be specified between 9 μm and 30 μm, depending on application requirements. Width dimensions are likewise fully customisable. The material surface exhibits a uniform metallic silver-white lustre, delivering both industrial robustness and aesthetic refinement without requiring additional finishing treatments.
Features
Barrier Performance and Structural Attributes
The defining performance attribute of ABL-Silver lies in its active defence against ambient environmental factors. The integrated aluminium foil acts as a dense, non-porous shield, providing intrinsic impermeability to light, oxygen, moisture and volatiles. Key functional outcomes include:
Complete light exclusion – the opaque nature of aluminium fully blocks ultraviolet and visible radiation, effectively preventing photo-induced degradation, colour fading, and loss of active ingredients in light-sensitive formulations.
Virtually zero permeability to gases and water vapour – the crystalline structure of aluminium renders the material impermeable to oxygen and steam, a critical feature for products requiring extended stability and shelf-life preservation.
Thermal reflectance and passive temperature moderation – the high reflectivity of the foil surface helps deflect incident radiant heat, offering supplementary thermal buffering during storage and transit.
From a mechanical standpoint, ABL-Silver demonstrates an optimal balance of stiffness and toughness. The multi-layer composite construction imparts superior tear strength and puncture resistance, enabling the packaging to withstand filling, stacking, and handling stresses throughout the supply chain while maintaining structural integrity. The material also exhibits sufficient rigidity for efficient automated tube-making and filling lines, with minimal risk of creasing or deformation.
Mechanical Performance and Process Compatibility
ABL-Silver is engineered for broad compatibility with downstream converting operations. Its surface is readily printable via letterpress, flexographic, screen, rotogravure processes, and supports both hot and cold foil stamping for high-impact decorative effects. The substrate accepts inks with excellent adhesion and colour fidelity, granting brand designers ample creative latitude in executing sophisticated graphics and metallic accents.
In tube-forming and sealing operations, ABL-Silver provides reliable heat-seal performance, producing consistently strong and uniform seals that prevent content leakage and external contamination. Whether using high-frequency welding or conventional thermal sealing, repeatable closure integrity is assured.
Applications
Principal Application Fields
Leveraging its balanced performance profile, ABL-Silver has been widely adopted across several consumer goods segments:
Food & condiments – ideal for packaging ketchup, mayonnaise, mustard, salad dressings, and similar products. The aluminium barrier effectively preserves original flavour and aroma profiles while preventing oxidative colour change and rancidity.
Oral care – extensively used for toothpaste tubes and dental adhesive packaging. The material exhibits chemical inertness towards active ingredients such as fluorides and antimicrobial agents, ensuring product stability over the intended shelf life.
Personal care & cosmetics – suited for hand creams, facial cleansers, hair dyes, and various emulsion- or gel-based cosmetics. The metallic silver appearance enhances shelf appeal, while the high barrier prolongs the efficacy of oxygen-sensitive actives (e.g., vitamin C, retinoids).
Household & industrial products – applicable to shoe polish, adhesives, sealants, and other chemical preparations. The aluminium layer provides excellent resistance to organic solvents and reactive compounds, safeguarding chemical stability.
Comprehensive Competitive Advantages
ABL-Silver establishes a clear differentiated advantage at the intersection of functional performance and commercial benefits:
Long-term freshness preservation and quality assurance – Leveraging the near-absolute barrier capability of the aluminium foil layer, the material provides reliable shelf-life support for food, pharmaceuticals, and highly active cosmetic formulations, effectively reducing loss risks associated with product degradation.
Reliable seal integrity and user confidence – Consistent heat-seal strength and high closure integrity ensure leak-proof performance throughout end-user handling, eliminating concerns over content leakage or external contamination.
Chemical inertness and broad media compatibility – The material exhibits outstanding corrosion resistance against acids, alkalis, alcohols, and a variety of chemical agents, making it suitable for packaging contents with complex compositions or mildly aggressive properties.
Visual premiumisation and brand enhancement – The inherent silver-white metallic finish conveys an immediate quality cue, while the excellent printability allows for high-definition graphics. Together, these attributes help brands project a premium image on retail shelves and reinforce consumer perception of product quality.
In essence, ABL-Silver is not merely a functional packaging film; it is a systematically engineered solution that integrates the ultimate protective properties of aluminium foil with the versatility of modern laminate manufacturing. It addresses the dual imperatives of preservation and presentation—offering robust, repeatable performance for demanding applications while enabling distinctive brand expression. For manufacturers seeking a packaging material that delivers uncompromising barrier protection without sacrificing design flexibility, ABL-Silver represents a proven, adaptable, and cost-effective choice.
Professional Service
Interested? Leave your contact details.
Search Starts Here