
‹
›
OEM Service Process
Complete the cooperation in four simple steps, with a professional team providing full support throughout the process.
Confirmation of product type, specifications, quantity, and special requirements
Provide a complete solution and detailed quotation
Make samples and adjust them to satisfaction
Mass production delivery based on confirmed samples
Product Detail
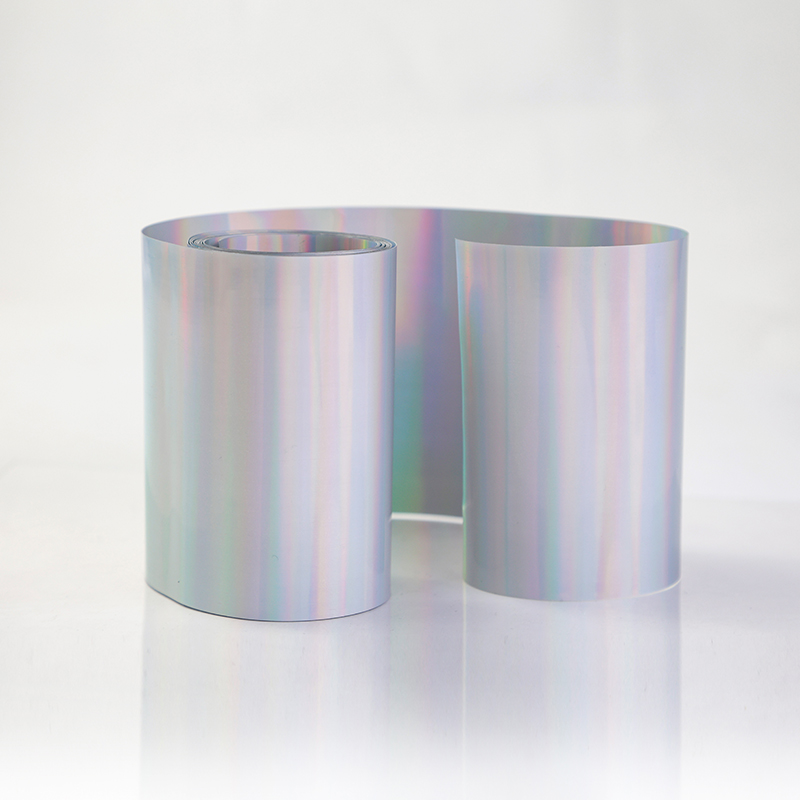
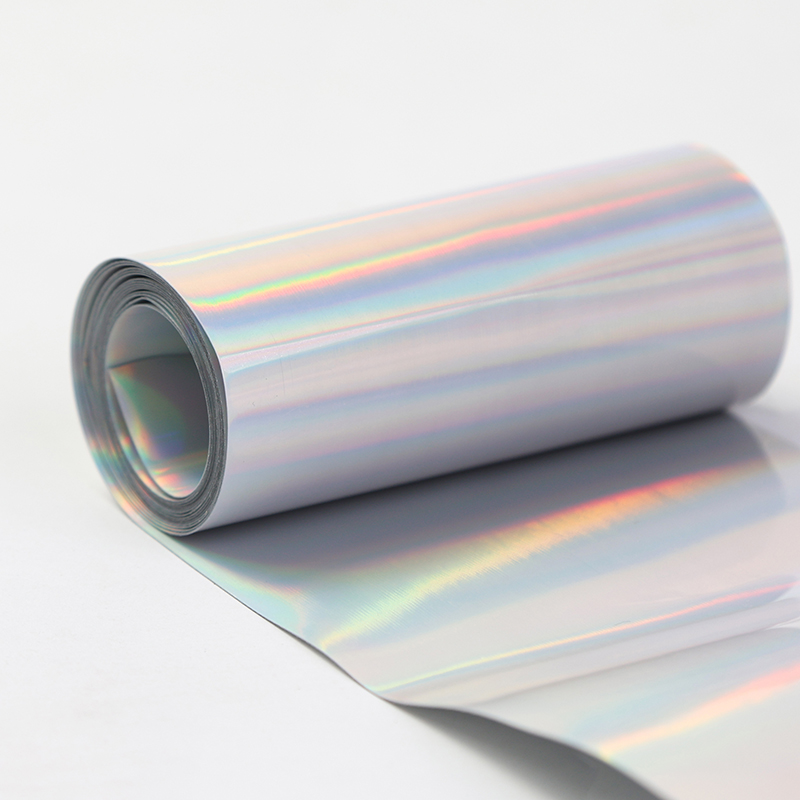
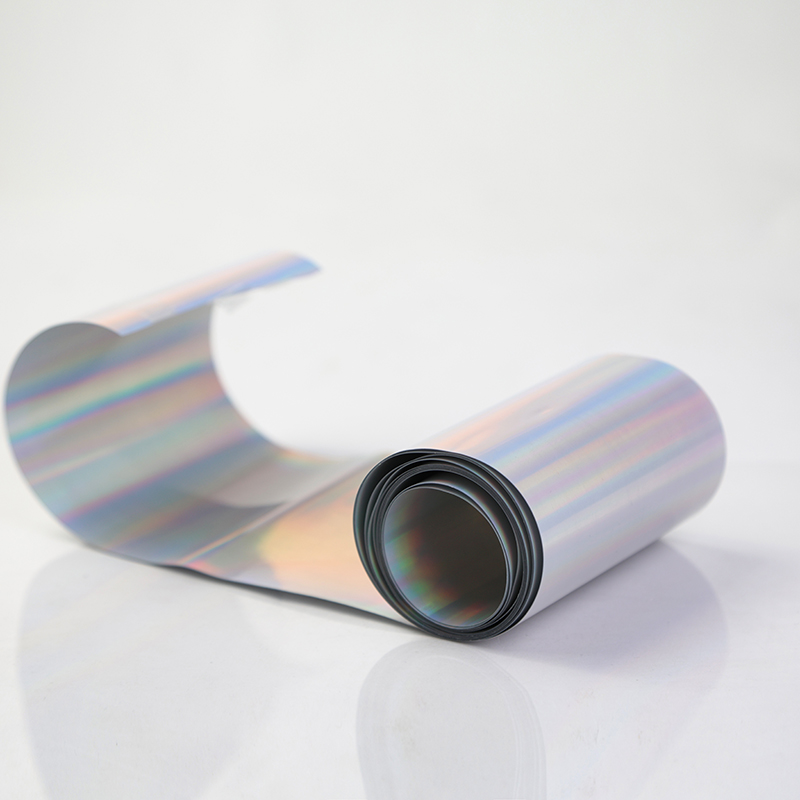
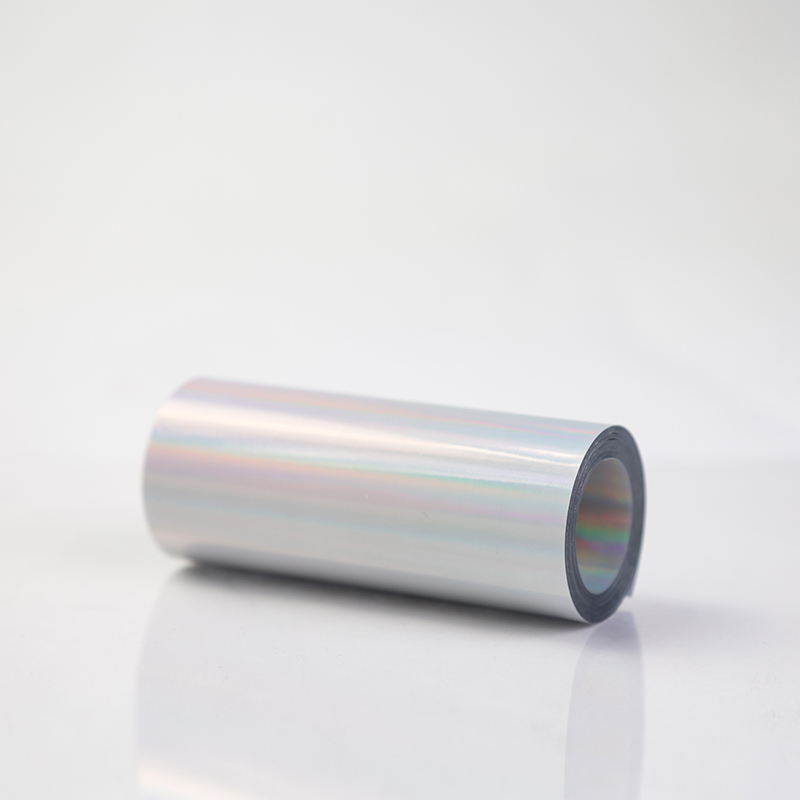
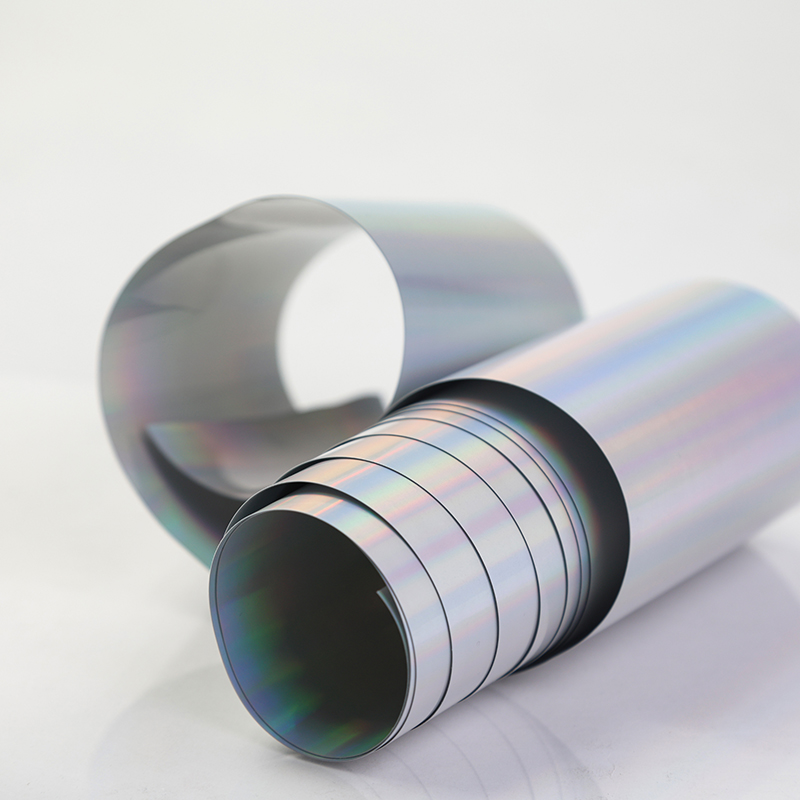
HAL (Holographic Aluminum Laminate) is a composite packaging web featuring a holographic film as its core visual layer. Through a multi‑layer co‑extrusion lamination process, the holographically embossed metallised film is integrated with polyolefin substrates to form a multi‑layer structure that delivers both dynamic optical effects and balanced physical properties. The holographic layer, through its precision micro‑grating structure, produces interference and diffraction of incident light, resulting in rich colour transitions and pattern variations that offer a highly recognisable visual language for premium packaging applications.
Total thickness is configurable within a range of 275 μm to 425 μm, with web width fully customisable per customer requirements. The material surface exhibits a high‑gloss finish and supports a comprehensive suite of printing technologies, including letterpress, flexographic, screen, rotogravure, and hot/cold foil stamping, accommodating diverse brand‑specific design needs.
Features
Barrier Performance and Structural Attributes
Holographic Optical Effects and Visual Performance-The defining differentiation of HAL originates from the dynamic optical effects delivered by its holographic layer:
Dynamic colouration and optically variable effects-The holographic layer, through its micro‑ and nano‑scale grating structures, produces interference and diffraction of light, resulting in rich colour gradations and shimmering effects that shift with varying viewing angles. This dynamic visual characteristic rapidly captures consumer attention at retail points of sale, imparting a pronounced sense of technological sophistication and luxury to the packaging.
Customisable patterns and brand identity integration-Holographic effects can be custom‑engineered to incorporate brand logos, proprietary motifs, or specific symbols directly into the grating structure. This enables the packaging to convey brand identification while delivering optical effects. Such customisation capability assists brands in establishing a distinctive visual identity within competitive markets, appealing particularly to young consumers who value individuality and contemporary aesthetics.
Innovative brand image empowerment-The holographic effect itself communicates an innovative, forward‑looking brand personality, making it suitable for premium brand image development and seasonal gift packaging applications. It effectively enhances shelf presence and brand equity.
Mechanical Performance and Process Compatibility
Protective Performance and Physical Properties - While delivering visual value, the metallised structure within HAL also serves a critical protective function. This construction provides effective shielding against oxygen, water vapour, and ultraviolet radiation, significantly mitigating the risk of product degradation caused by oxidation, moisture ingress, or photo‑induced reactions, thereby supporting quality maintenance throughout the shelf‑life period. This characteristic is particularly critical for cosmetic and skincare products containing active ingredients.
In terms of physical properties, HAL features a multi‑layer composite construction that imparts excellent tear resistance, abrasion resistance, and flex‑crack resistance to the web. The material effectively preserves packaging container integrity throughout tube‑forming, filling, stacking, and transportation phases, while accommodating diverse complex or irregular packaging configurations.
Regulatory Compliance and Process Compatibility - The raw materials selected for HAL comply with international cosmetic and food‑contact safety standards; they are non‑toxic and odourless, making the material suitable for packaging applications involving direct content contact.
In terms of process compatibility, HAL can be flexibly combined with multiple downstream processes, including foil stamping, lamination, and printing, to accommodate diversified production line requirements, contributing to reduced overall production costs and enhanced operational efficiency.
Applications
Principal Application Fields
Premium cosmetic packaging-suitable for tube‑packed products including serums, sunscreens, eye creams, and foundations. The holographic effect aligns closely with the luxury‑technology positioning of high‑end skincare brands, significantly enhancing shelf presence and brand recognition.
Premium oral care products-suitable for outer packaging of premium toothpaste tubes. The holographic optical effect imparts a renewed visual experience and quality perception to traditional product categories.
Comprehensive Competitive Advantages
HAL delivers tangible value to professional purchasers across optical effects, protective functionality, and process compatibility:
Distinctive optical effects enhance visual impact-dynamic colour transitions and optically variable effects; customisable patterns support brand logo and proprietary symbol integration; significantly improves product recognition and shelf competitiveness.Reliable protective performance-effective shielding against oxygen, water vapour, and ultraviolet radiation, preserving quality stability of contents containing active ingredients.
Superior process compatibility-flexible combination with foil stamping, lamination, printing, and other downstream processes; accommodates diversified production line requirements; effective control of overall production costs.
HAL is a packaging substrate that deeply integrates holographic optical effects with a composite packaging structure. Its holographic layer, through precision grating structures, delivers dynamic colour transitions that construct a highly recognisable visual language for brands; concurrently, the metallised structure provides reliable protection for contents. For international brand owners seeking to achieve brand differentiation through packaging innovation and establish a technologically sophisticated, luxurious image in the premium market segment, HAL represents a choice of outstanding aesthetic innovation and technical reliability.
Related Products
 ABL-Silver High-Barrier Aluminum Laminate Packaging Material
 ABL-White-High-Whiteness Aluminum Barrier Laminate Web for Premium Packaging Applications
 APL-Transparent-All-Plastic Transparent Laminate Web-EVOH-Free High-Barrier Eco-Friendly Packaging Substrate
 APL-White-All-Plastic White Laminate Web-EVOH-Free High-Whiteness Eco-Friendly Packaging Substrate
 CAL-Metalised Laminate Web-High-Gloss Mirror-Effect Premium Packaging Substrate
 HAL-Holographic Laminate Web-Dynamic Optical-Effect Premium Packaging Substrate
 PBL-Transparent-All-Plastic Transparent Laminate Web-EVOH-Containing Premium Transparent Packaging Substrate
 PBL-White-All-Plastic White Laminate Web-EVOH-Containing, AL-Free Eco-Friendly Substrate
Professional Service
Interested? Leave your contact details.
Search Starts Here