
‹
›
OEM Service Process
Complete the cooperation in four simple steps, with a professional team providing full support throughout the process.
Confirmation of product type, specifications, quantity, and special requirements
Provide a complete solution and detailed quotation
Make samples and adjust them to satisfaction
Mass production delivery based on confirmed samples
Product Detail
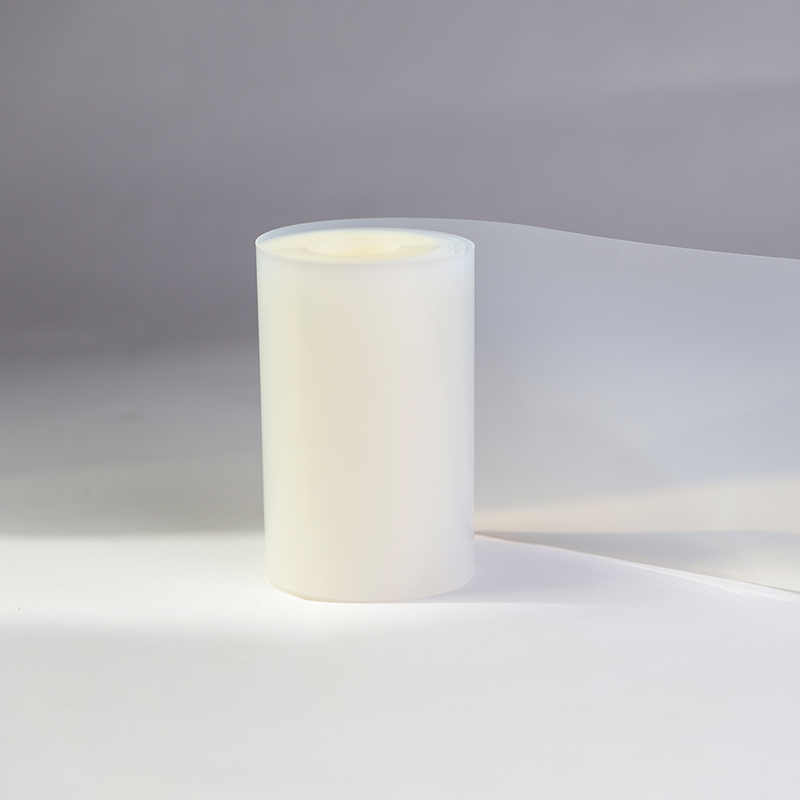
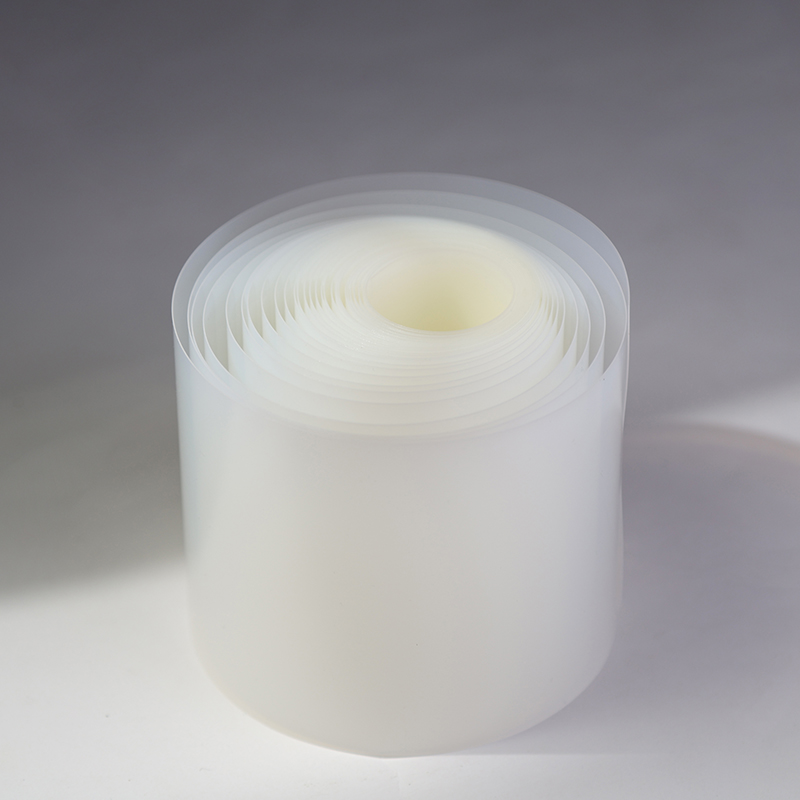
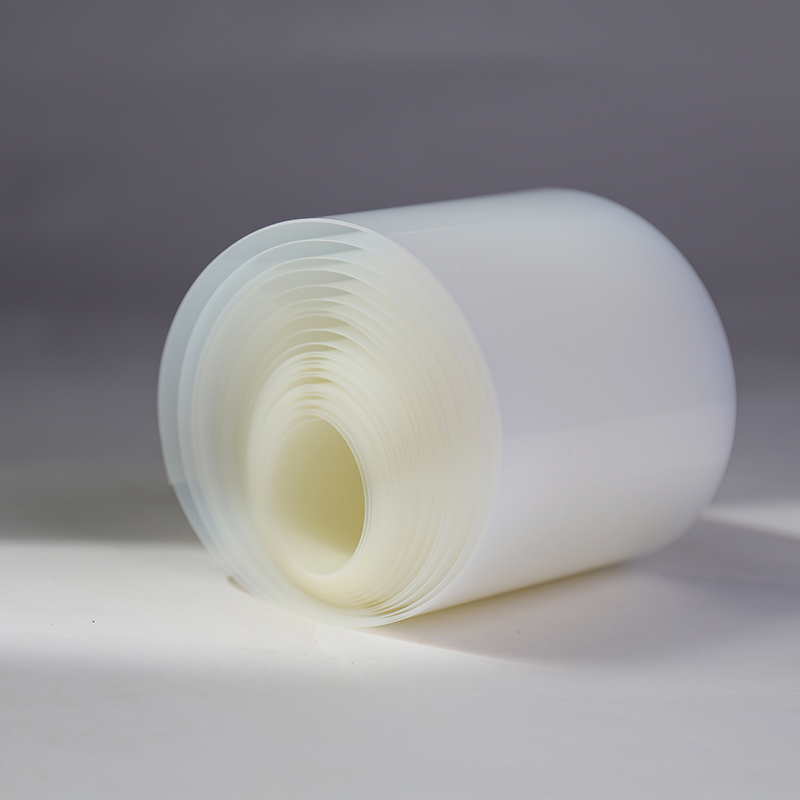
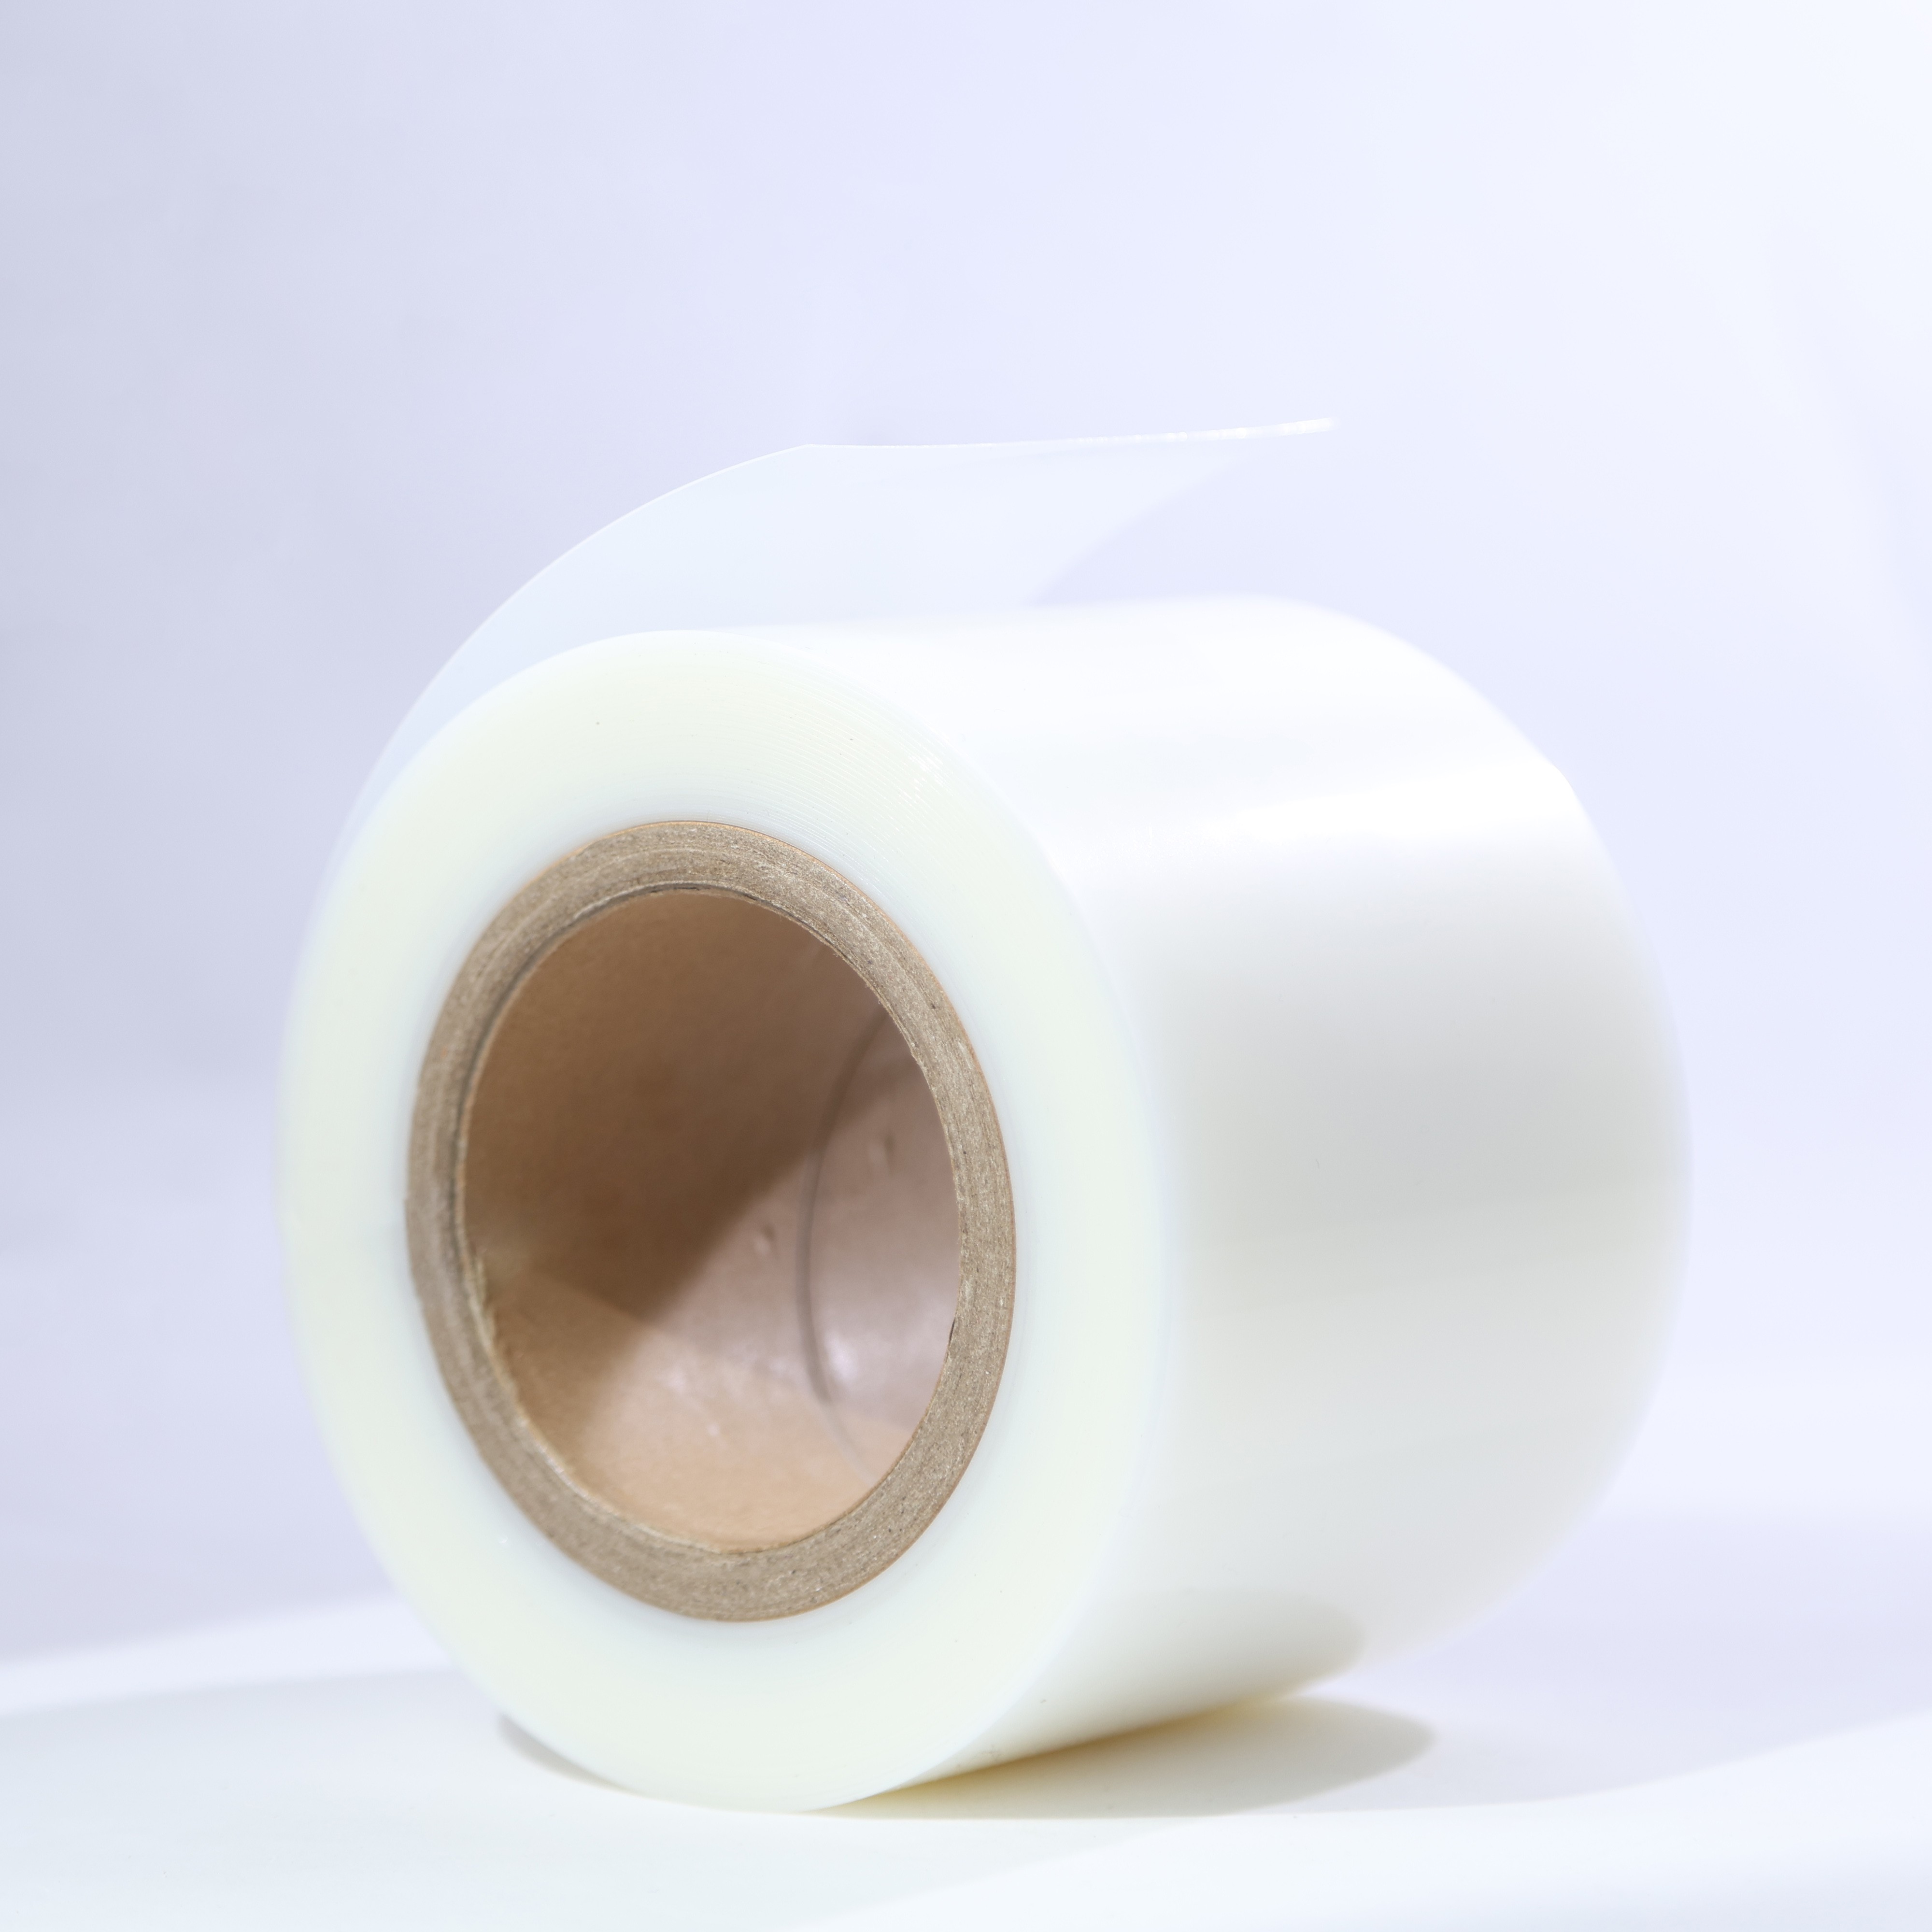
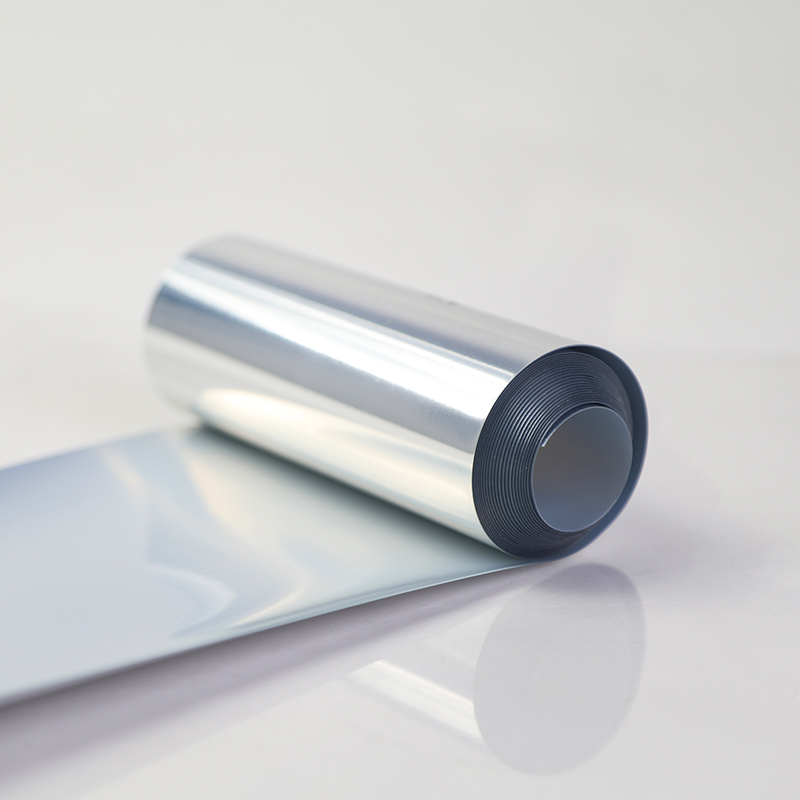
PBL‑Transparent is a fully transparent composite packaging web manufactured via multi‑layer co‑extrusion technology, formulated with EVOH (ethylene‑vinyl alcohol copolymer) incorporated as the core functional barrier layer. The product is strategically positioned for the premium packaging segment, combining the recyclability of an all‑plastic structure with significantly enhanced oxygen‑shielding performance—superior to conventional polyolefin materials—through the integration of the EVOH layer. It offers a packaging solution that delivers both protective performance and visual transparency for food, cosmetic, and oral care products with stringent shelf‑life and content‑stability requirements.
Total thickness is configurable within a range of 250 μm to 425 μm, with web width fully customisable per customer requirements. In terms of appearance, PBL‑Transparent maintains the inherent optical clarity of the substrate, allowing end‑packaging to clearly display the colour, texture, and form of the contents, thereby maximising the inherent visual appeal of the product itself. The material supports a comprehensive suite of decoration processes, including letterpress, flexographic, screen, rotogravure, and hot/cold foil stamping, enabling brand expression at a premium level while preserving transparency.
Features
Barrier Performance and Structural Attributes
The defining technical attribute of PBL‑Transparent lies in its incorporation of an EVOH barrier layer. EVOH, as a copolymer characterised by high molecular chain regularity, exhibits strong intermolecular forces and low free volume, resulting in a pronounced suppressive effect on the permeation of oxygen and other gaseous molecules. Within the multi‑layer co‑extruded architecture, the EVOH layer is typically positioned between inner and outer polyolefin protective layers. Through optimised thickness ratios and layer arrangement, the material attains superior oxygen‑protection capability, effectively retarding oxidative degradation—including colour changes, flavour loss, and nutrient depletion—of packaged contents.
Notably, the EVOH layer does not compromise the transparency of the material. PBL‑Transparent achieves excellent protective performance while maintaining outstanding optical clarity, enabling concurrent fulfilment of protective and display functions. In terms of moisture protection, the outer polyolefin layers provide a reliable water‑vapour barrier, ensuring a balanced performance profile across both oxygen‑protection and moisture‑resistance dimensions.
Mechanical Performance and Process Compatibility
Mechanical Properties and Chemical Resistance
PBL‑Transparent demonstrates robust mechanical strength attributes. The multi‑layer co‑extruded construction imparts excellent impact resistance and puncture resistance, effectively preserving packaging container integrity throughout filling, stacking, and transportation phases. The inherent toughness of the material ensures stable performance on automated high‑speed tube‑forming and filling lines, minimising process defects such as film rupture or cracking.
From a chemical resistance standpoint, EVOH exhibits good oil resistance and resistance to chemical solvents. This characteristic enables PBL‑Transparent, when packaging oil‑containing contents (e.g., mayonnaise, salad dressings, hand creams), to effectively resist the permeation and attack of oils and organic components on the barrier layer, thereby ensuring sustained protective functionality throughout the intended shelf life. Additionally, the chemical inertness of the material mitigates the risk of adverse interactions between packaging material and contents.
Heat‑Seal Performance and Tube‑Forming Compatibility
PBL‑Transparent employs a PE‑based sealant layer, delivering robust heat‑seal strength and reliable closure integrity. In tube‑forming operations, the material feeds smoothly through both intermittent and continuous tube‑forming equipment, offering a broad sealing window that permits stable seal performance across a wide range of process parameters. Seal integrity is a critical quality indicator, directly governing the leak‑proof and contamination‑prevention capabilities of the finished package.
Applications
Principal Application Fields
Food packaging-suitable for tube‑packed oil‑containing or semi‑liquid condiments such as ketchup, mayonnaise, mustard, and salad dressings. The high transparency enables consumers to directly visualise the contents, while oxygen‑protection performance effectively prevents oxidative rancidity of oils, extending flavour shelf life.
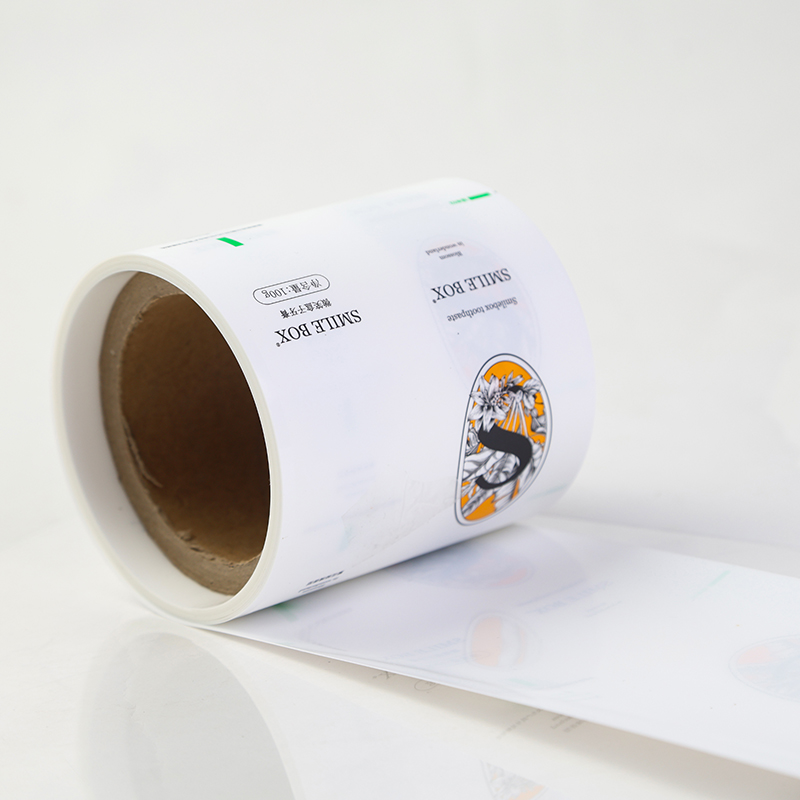
Oral care products-applicable to toothpaste, dental adhesives, and similar oral hygiene products. The transparent tube body reveals the colour and texture of the formulation, assisting brands in communicating product attributes.Cosmetics and personal care-suitable for hand creams, facial cleansers, hair dyes, and a variety of emulsion‑ and gel‑based cosmetic products. The combination of high transparency and superior protective performance protects active formulations (e.g., vitamin C, retinoids) while enhancing shelf appeal through transparent product presentation.
Comprehensive Competitive Advantages
PBL‑Transparent delivers tangible value to professional purchasers across protective performance, visual presentation, and structural reliability:
Superior protective performance-incorporating an EVOH barrier layer with extremely low oxygen transmission rates, significantly extending content shelf life; outer polyolefin layers simultaneously provide a moisture barrier, achieving a balanced configuration of oxygen‑protection and moisture‑protection.
Premium visual quality-inherent high transparency, clearly showcasing the colour and texture of contents; supports multiple printing processes and colour designs, aligning with the packaging requirements of luxury and high‑end brands.
Robust structural durability-excellent impact and puncture resistance; good resistance to oils and chemical corrosion; effectively safeguards product safety and quality throughout storage, distribution, and end‑use cycles.
PBL‑Transparent is a premium packaging substrate that deeply integrates EVOH's exceptional protective functionality with all‑plastic transparent aesthetics. Through its multi‑pronged defence against oxygen, moisture, and chemical attack, it provides reliable protection for contents with demanding preservation requirements; concurrently, its high transparency transforms the product itself into a visual focal point on retail shelves. For international packaging buyers seeking to achieve both protective excellence and brand prestige, PBL‑Transparent represents a technologically advanced and market‑differentiated choice.
Related Products
 ABL-Silver High-Barrier Aluminum Laminate Packaging Material
 ABL-White-High-Whiteness Aluminum Barrier Laminate Web for Premium Packaging Applications
 APL-Transparent-All-Plastic Transparent Laminate Web-EVOH-Free High-Barrier Eco-Friendly Packaging Substrate
 APL-White-All-Plastic White Laminate Web-EVOH-Free High-Whiteness Eco-Friendly Packaging Substrate
 CAL-Metalised Laminate Web-High-Gloss Mirror-Effect Premium Packaging Substrate
 HAL-Holographic Laminate Web-Dynamic Optical-Effect Premium Packaging Substrate
 PBL-Transparent-All-Plastic Transparent Laminate Web-EVOH-Containing Premium Transparent Packaging Substrate
 PBL-White-All-Plastic White Laminate Web-EVOH-Containing, AL-Free Eco-Friendly Substrate
Professional Service
Interested? Leave your contact details.
Search Starts Here